How to Choose the Best PCB Assembly Equipment?
Oct 23, 2026
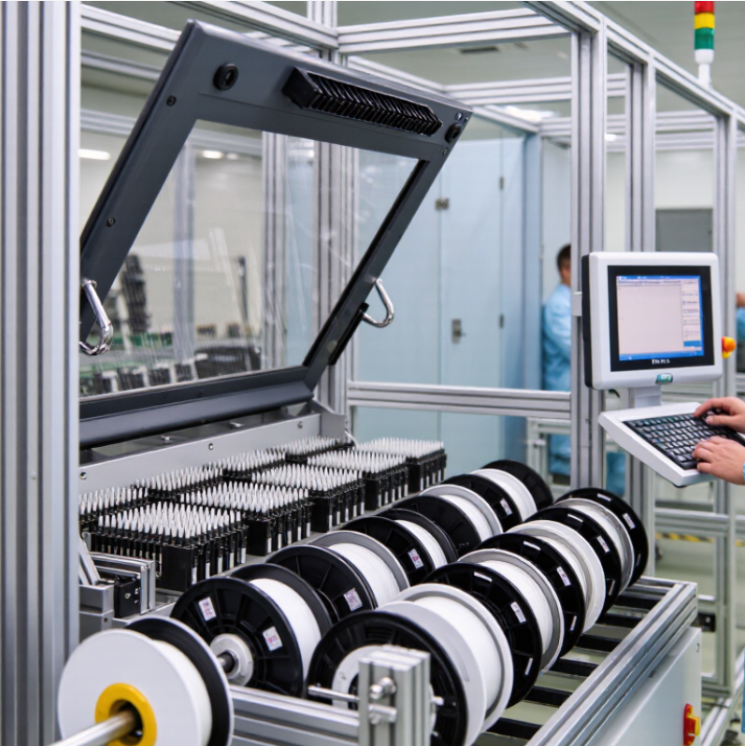
Shenzhen, Guangdong Oct 22, 2026 (Issuewire.com) - Choosing the right Pcb Assembly Equipment is rarely a simple comparison of speed and price. A machine may promise 60,000 placements per hour, yet produce disappointing output when feeders, nozzles, or software are poorly matched. Real performance appears on the factory floor. It appears during product changeovers, feeder loading, inspection, and maintenance.
Michael Ford, Senior Technical Manager at Aegis Software, states, "Technology should solve a manufacturing problem, not create another one." This principle deserves attention. A fast placement machine cannot compensate for weak production data or unreliable material control. Buyers should examine placement accuracy, component range, changeover time, feeder capacity, and integration with MES platforms. They should also evaluate Smt Assembly Equipment as part of one connected process, not as isolated machines.
Look closely.
A practical evaluation should include sample boards, difficult components, and realistic production volumes. Ask suppliers to demonstrate fine-pitch placement, small passive components, odd-form parts, and traceability records. Inspect the software interface, alarm clarity, spare-parts policy, and local technical support. These details often affect daily productivity more than impressive brochure figures.
There is also room for doubt. The newest equipment is not always the best investment. A mid-range system may deliver stronger value when operators can learn it quickly and engineers can service it locally. Energy use, future product changes, factory space, and training costs deserve equal attention. The final decision should connect measurable production needs with dependable long-term support. A careful buyer does not chase speed alone. Reliability usually wins.
Understanding PCB Assembly Equipment and Its RoleHow to Choose the Best Pcb Assembly Equipment?
Understanding the role of PCB Assembly Equipment is more important than choosing the newest machine. In a working production line, each system affects placement accuracy, solder quality, speed, and traceability. A stencil printer controls paste volume at the beginning. A pick-and-place machine positions components with measured precision. The reflow oven then manages heat across several temperature zones. Small changes matter. A few extra degrees can damage sensitive parts or create weak solder joints.
Experience shows that equipment should match the product, not only the expected output. A compact board with fine-pitch components needs accurate vision systems and stable feeders. A high-mix workshop may need fast changeovers and flexible software.
SPI and AOI equipment can identify paste defects, missing components, and alignment problems before they become expensive failures. ESD protection, maintenance access, spare parts, and operator training also influence reliability. I once focused too heavily on speed and underestimated feeder setup time. That decision looked efficient on paper, but production became slower.
Tips: Record your real cycle time. Check service access. Test difficult components before purchasing. Ask suppliers for sample results and maintenance details. Leave room for process mistakes; perfect planning is uncommon. Review noise, heat, and floor space as well. Operators notice practical problems that specifications often miss. A machine may meet its accuracy rating, yet still feel unsuitable during a long shift. Feedback from technicians should therefore shape the final choice.
Defining Production Requirements and Assembly GoalsHow to Choose the Best PCB Assembly Equipment?
Defining production requirementsshould come before comparing machines. Start with the board's dimensions, layer count, component mix, and expected monthly volume. A compact Prototype Board needs different equipment from a high-volume controller with fine-pitch packages. Record the smallest components, tallest parts, connector types, and placement tolerances. These details influence feeder capacity, nozzle selection, inspection methods, and reflow control.
Set measurable assembly goals. Target throughput, placement accuracy, first-pass yield, changeover time, and traceability. If your production includes frequent design changes, flexible programming may matter more than maximum speed. For stable production, automated material handling can reduce repetitive errors. Define acceptable solder defects and inspection coverage before selecting equipment. A vague goal creates expensive compromises. I have seen teams prioritize speed, then discover that manual verification slows every completed panel.
Tips:
Build a simple requirement sheet. Include board size, component range, daily output, staffing, and available floor space. Test sample boards under realistic conditions. Include difficult parts, not only easy ones. Ask whether operators can maintain the equipment safely and consistently. A perfect specification may still fail when changeovers are frequent. Leave room for learning. Production rarely follows the first spreadsheet.
Comparing Equipment Types for Different PCB Processes
Choosing Electronic Assembly Equipment starts with the PCB process, not the machine catalog. In a small prototype line, a manual stencil printer, compact pick-and-place unit, and benchtop reflow oven can control costs. Operators can adjust feeders quickly. They can also observe solder paste changes directly. This setup suits short runs and frequent design revisions. However, placement speed remains limited. That trade-off is easy to underestimate.
For steady SMT production, automatic printers and high-speed placement systems improve repeatability. A reflow oven with several thermal zones protects solder joint quality across changing board sizes. Inline optical inspection finds missing components, skewed parts, and insufficient solder. Use X-ray inspection when hidden joints or dense packages create uncertainty. Inspection is not decoration. It protects process data. Yet, excessive automation can complicate maintenance and slow a simple job.
Through-hole assemblies need different tools. Lead-forming equipment, insertion machines, selective soldering systems, and capable hand-soldering stations support larger terminals and heavier components. Mixed-technology boards may require SMT and through-hole equipment, plus a controlled rework station. In my experience, the best choice balances takt time, board variety, floor space, and operator skill. I once favored faster placement, then found feeder changes consumed the expected gain. Measure real cycle time, not brochure speed. Leave room for calibration, cleaning, and the occasional mistake.
Evaluating Capacity, Precision, Speed, and Flexibility
Choosing PCB assembly equipment starts with production evidence, not brochure capacity. Review weekly board volume, package mix, changeover frequency, and operator workload. A machine rated for 50,000 placements per hour may slow with tiny components and frequent feeder adjustments. Measure the bottleneck. Surface Mount Equipment should match your real takt time, including loading, inspection, and rework pauses. Leave capacity headroom for seasonal orders, but avoid paying for idle speed.
Precision needs practical testing. Ask for placement accuracy data across fine-pitch packages, small passives, and uneven boards. Examine solder paste printing, component placement, and optical inspection as one connected process. A precise placer cannot rescue poor stencil alignment. Check sample panels from your factory, not only demonstration boards. Inspect first-off units under magnification, then compare defect rates after several hours. Small details matter. Equipment does not stay perfectly calibrated, so maintenance access and calibration records affect reliability.
Speed matters when it remains stable during changeovers. Flexible equipment should support different board sizes, component ranges, feeders, and software recipes without complicated resets. A quick setup is valuable, but rushed setup creates hidden defects. Consider training time, spare-part availability, data tracking, and operator safety. I have seen lines lose more output through feeder confusion than slow placement. That experience is uncomfortable. It also challenges simple purchasing calculations. Trial the complete workflow before approval, and record changeover minutes, first-pass yield, and unplanned stops under normal production conditions.
Checking Compatibility with Components, Materials, and Software
Choosing PCB assembly equipment begins with the component library, not the machine catalog. Confirm package sizes, lead spacing, board thickness, and component height. A feeder designed for 0201 parts may still struggle with warped tape or fragile terminals. IPC's 2024 Electronics Industry Impact Report valued global electronics production at approximately $5.1 trillion, showing how small compatibility errors can scale into serious losses.
Materials require equal attention. Check solder paste chemistry, substrate finish, copper weight, and maximum reflow temperature. IPC-7095 guidance highlights thermal and design challenges around area-array packages. The wrong profile can create voids beneath large thermal pads or damage moisture-sensitive components. I have seen teams trust a standard profile too quickly. That assumption needs testing. Run thermal profiling on the actual board, not only on a supplier's sample.
Software compatibility is easier to underestimate. Equipment should exchange CAD, centroid, bill-of-materials, and inspection data without repeated manual conversion. The IPC Connected Factory Initiative emphasizes interoperable manufacturing data, while the NIST Cybersecurity Framework 2.0 recommends managing technology risks across connected systems. Verify file formats, revision control, permissions, and traceability before purchasing. A machine may advertise broad compatibility, yet still reject a minor library variation. Perform a pilot build using difficult components, real materials, and the intended software workflow. Record placement accuracy, changeover time, solder defects, and operator corrections. The result may challenge the original equipment shortlist.
Assessing Total Costs, Maintenance, and Operator Requirements
Choosing PCB assembly equipment requires more than comparing purchase prices. In Electronic Equipment Manufacturing, the real cost appears during daily operation. A machine may cost $40,000, yet tooling, feeders, software updates, electricity, and installation can add thousands more. Ask for a five-year cost estimate. Include spare parts, calibration, training, and production downtime.
Maintenance needs practical evaluation. Check how often nozzles, belts, filters, and sensors require replacement. A technician should access these parts without dismantling half the machine. Request maintenance records from current users, not only supplier forecasts. One missed calibration can create solder defects across hundreds of boards. I have seen teams underestimate this risk. Their budget looked accurate, but repairs delayed production for three days.
Tips: Watch a live demonstration with your own board files. Time setup changes between two product types. Ask operators to complete basic tasks, such as feeder loading and error recovery. Their feedback often reveals hidden complexity. Short training is valuable. Clear screens matter more. Also, calculate operator requirements per shift, including inspection and material handling. A system requiring one skilled specialist may become expensive when that person is absent. Some evaluations fail here. Mine probably would too, without a documented backup plan.
Radiation Detector PCB Assembly: Key Design, Components, and Manufacturing Considerations
A radiation detector PCB assembly serves as the ionizing radiation sensing core in environmental and industrial monitoring equipment. Its design must support the detection of alpha, beta, gamma, and X-ray radiation while maintaining stable performance under demanding conditions. Key considerations include low-noise circuit layout, controlled impedance, effective grounding, shielding, and separation between sensitive analog paths and digital processing sections. These measures help improve detection sensitivity, reduce electromagnetic interference, and limit false alarms caused by electrical noise or temperature variation.
The assembly typically integrates a radiation sensor interface, signal amplification and conditioning circuits, analog-to-digital conversion, a microcontroller, memory, power regulation, and communication interfaces. Carefully selected components allow weak sensor signals to be amplified without distortion, while embedded dose calculation algorithms convert pulse or energy data into useful real-time radiation readings. Temperature compensation and calibration functions can further improve measurement consistency across changing environments.
Manufacturing quality is equally important. Controlled soldering profiles, clean assembly processes, Automated Optical Inspection, electrical testing, and functional calibration help identify component placement errors, solder defects, and signal instability. Protective coatings or mechanical shielding may be added when the PCB operates in humid, dusty, or vibration-prone locations. With reliable assembly and verification, the detector can support radiation monitoring in nuclear power facilities, medical institutions, geological exploration projects, and environmental monitoring stations, providing timely dose information and safety alerts.
Conclusion
Choosing the right Pcb Assembly Equipment is essential for achieving stable quality, efficient production, and long-term manufacturing value. The selection process should begin by defining production requirements, including PCB size, expected output, product complexity, assembly goals, and future expansion plans. Different processes may require different equipment types, so manufacturers should compare solutions according to placement, soldering, inspection, handling, and rework needs.
Key evaluation criteria include capacity, positioning precision, operating speed, changeover efficiency, and flexibility for varied product designs. Equipment must also be compatible with the components, board materials, soldering methods, software systems, and data formats used in the production environment. Beyond the purchase price, it is important to assess total ownership costs, energy use, maintenance schedules, spare parts, training, and operator requirements. A well-balanced decision will support reliable performance, simplify daily operations, reduce downtime, and provide a practical foundation for consistent PCB assembly as production demands evolve.
Source :Shenzhen STHL Electronics Co., Ltd.
This article was originally published by IssueWire. Read the original article here.
More News



YOUR NEWS, OUR NETWORK.
Do you have Great News you want to tell the world?
Be it updates about your business or your community, you can make sure that it’s heard by submitting your story to our network reaching hundreds of news sites across 6 verticals.